The Physics of Threaded NPT Gas Joints
In residential gas systems throughout Ashburn Farm, Ashburn Village, and Sterling, black iron fuel piping relies on National Pipe Taper (NPT) threads cut at a 1° 47′ taper angle. As male and female threads are screwed together, the taper wedges the thread crests and roots together to form a mechanical seal.
However, spiral clearance paths inherently exist between the mating thread flanks. To fill these microscopic channels, a high-grade pipe joint compound (pipe dope) containing PTFE fluoropolymer or specialized gas-rated yellow thread tape must be applied. Over 20 to 30 years, two phenomena cause these joints to fail:
- Drying & Embrittlement: Early petroleum-based joint dopes cure into brittle solids that crack when foundation settlement or pipe vibration shifts the manifold.
- Seasonal Thermal Contraction: During cold Loudoun County winters, outdoor meters and cold basement pipes contract, opening microscopic fissures that release detectable mercaptan odor.
Threaded Black Iron Pipe Joint & Sniffer Detection
This technical cutaway illustrates how microscopic thread sealant voids allow gas molecules to escape into living spaces, and how our digital sniffers detect parts-per-million concentrations:
Threaded Black Iron Pipe Joint & Gas Sniffer Detection
Cutaway showing tapered NPT male/female thread seal, microscopic fissure path, and electronic sniffer sensor detecting PPM mercaptan gas.
Prohibited DIY Repairs & Temporary Clamps
Under Virginia Fuel Gas Code § 406.4, external sealant pastes, silicone, rubber radiator clamps, and epoxy wraps are strictly prohibited on fuel gas piping. Fuel gas under pressure will eventually dissolve or channel through surface-applied adhesives, leading to catastrophic gas buildup behind walls.
Additionally, attempting to simply tighten an existing leaking joint with pipe wrenches often creates dangerous lateral torque, twisting and fracturing adjacent elbows or brittle water heater manifold connections upstream. A joint cannot be permanently fixed from the outside—it must be disassembled, cleaned, and properly reassembled.
Code-Compliant Joint Reconstruction Procedure
Our licensed master gas fitters follow an uncompromising repair protocol:
- System Isolation: Supply valves are turned off, and the localized line section is vented to the exterior.
- Opposing Wrench Disassembly: Using two heavy-duty rigid pipe wrenches (one backing up the fitting and one turning the pipe), the joint is disassembled without stressing adjoining lines.
- Wire Brush Thread De-Scaling: Old dried dope, rust scale, and debris are completely removed from male and female threads using steel wire brushes and solvent degreaser.
- Inspection of Thread Integrity: Threads are examined for cross-threading, galling, or stress cracks. Damaged sections are cut clean and freshly re-threaded on-site with handheld pipe dies.
- Application of Modern Anaerobic PTFE Sealant: We apply commercial-grade anaerobic pipe sealant engineered specifically for natural gas and LP, followed by 3 to 4 wraps of Mil-Spec gas PTFE tape.
- Precision Torquing & Alignment: The connection is torqued to manufacturer specifications, ensuring perfect pitch and alignment.
Electronic PPM Sniffing vs. Bubble Solution
Once reassembled, we verify joint tightness using a dual-testing protocol. First, the lines are pressurized with air to 15 PSI and treated with a high-viscosity, non-corrosive bubble leak detector (ASTM C1588 compliant). This solution forms long-lasting micro-bubbles on even the slowest seepage.
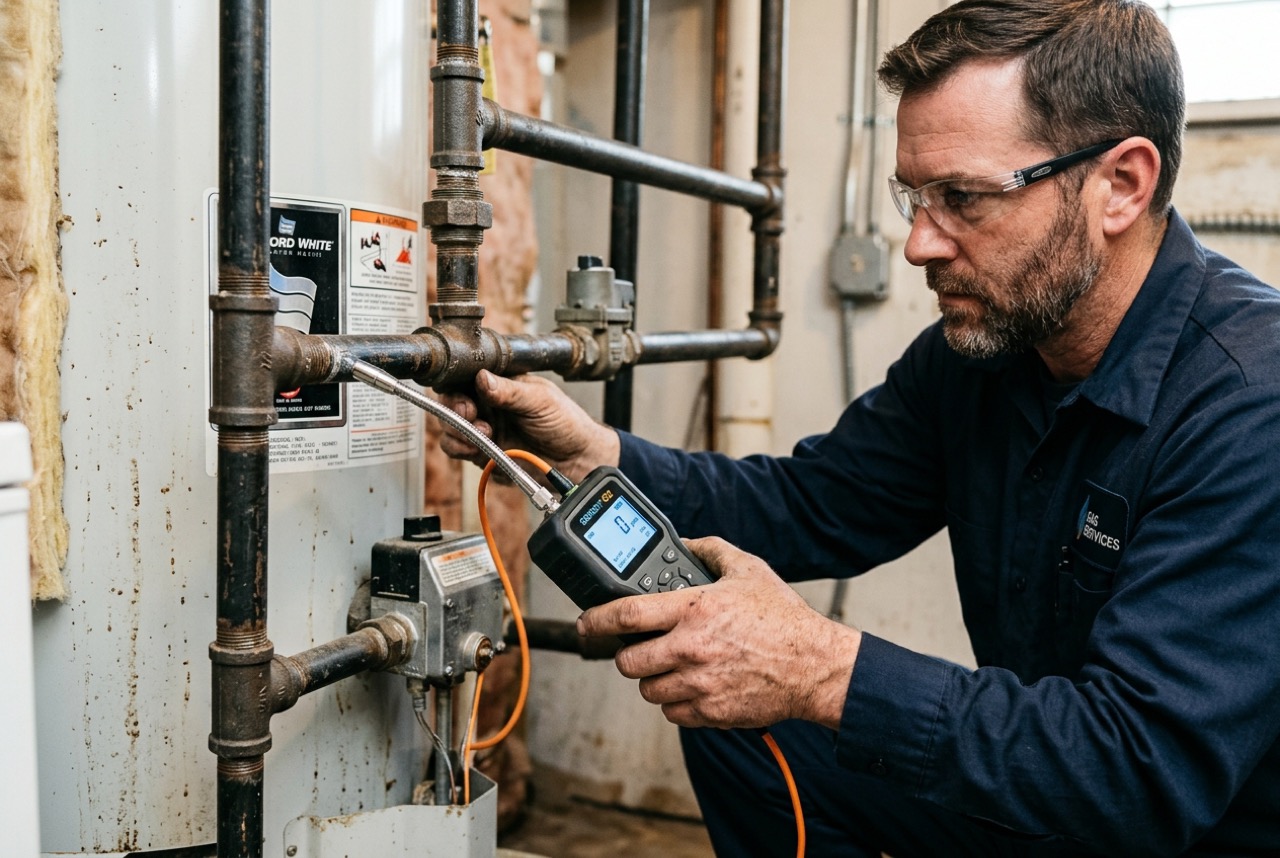
Second, after gas reintroduction, we scan the entire circumference of every joint using an intrinsically safe digital catalytic bead sniffer probe capable of resolving down to 10 parts per million (PPM) of methane, confirming zero residual leakage.
Smelling Gas Near Your Basement Pipes? Do not ignore intermittent odors. Call Ashburn Gas Response at (703) 312-2655 for precision sniffer diagnostics and code-certified joint resealing.